In 2016 we asked the Twitterverse to play along as we wrote sprayer poems in the form of haiku. The response was tremendous and the poems were so well done. We scooped them up into an article called #SprayerHaiku.
Well, we couldn’t help ourselves. On a nostaglic impulse, we did it again in 2017 and our Twitter followers rose to the occasion with a new batch of thoughtful Haiku! While we admit that a few people miscounted the syllables (5-7-5) their efforts make them worthy of a reprint.
The best submission, @HortGuy85, won a Sprayers101 Mug! It was his Yoda meme that put him over the top. You’ll have to read all the way to the end to see it.
Do I spray or not Follow thresholds for guidance Not rocket science (@TraceyBaute)
Have pesticide spill? Protect yourself first and call Spills Action Centre. (@ONspraysafety)
Two sprayer experts With a new mug up for grabs Making poets of farmers (@megnmoran)
Keep out after spray Restricted Entry Interval Tell others always (@ONspraysafety)
When spraying your crop, Don’t forget to #MixItUp Spray multiple Groups (@Bayer4CropsCa)
Modify water, use the proper adjuvants, droplet on target (@edakag1)
(To the tune of Red Solo Cup) Their green soybeans cupped, I shouldn’t have filled you up, Their lawyers’ party! (@ZRAgri)
Fine droplets drift off Float on the pre-dawn still air Keeping me employed (@Spraydriftgirl)
Dicamba Nozzles: Use TTI Ultra Coarse Xtend the boom (@Johannaburrows)
I know two rinses After spraying Odyssey Still nukes Canola (@DavidKucher)
Roses are red, Violets may be blue, They need spraying too (@HortResearchKTT)
Assume tomatoes Will be injured if even They smell dicamba (@ontariotomato)
Spray on autosteer but watch for field obstacles ****, down for repairs (@ontariotomato)
Driving sprayer fast Does not save as much time as Filling, cleaning fast.
Sprayer slows at turn, Pressure drops, gaps in the spray. Minimum 2 bar.
Dry, still, cloudless eve Why did my pesticide drift? Thermal inversion.
Single tank rinse After spraying dicamba Too much residue
Contorted will be Your berry growing career If Tordon you use (@HortGuy85)
Before we dive into the details, let’s start with a quick video summary filmed by RealAgriculture at Canada’s Outdoor Farm Show in September, 2016.
When the pressure drops and the nozzles begin to sputter, the sprayer is considered empty. However, it can still retain a lot of spray solution. Repeated rinses or tank dumps in the same location can lead to accumulation and cause point source contamination.
In response to unacceptably high levels of environmental pesticide contamination, the European Union published an amendment to their directive regarding machinery for pesticide application (2009/127/EC). Their intention was to raise the standard of equipment design to reduce the standing volume of spray solution, and to improve cleaning practices. In order to comply, sprayer technology and operator practices would have to change. But the the amendment didn’t specify how, or to what level.
France (2006) and Denmark (2009) legislated that a rinsed sprayer must not have more than 1% or 2%, respectively, of the original tank mix concentration, as sampled at the nozzle. In response, P G Anderson et al. suggested that residual concentrations should be sampled from at least three places on the sprayer. They conducted research (download here) that showed that both field and airblast sprayers can retain 10-15% of the original concentration in the empty/fill valves, boom ends and filters, while rinsate measured 1-2% at the nozzle. They also stated that in order for sprayer designers, operators and authorities to comply with these new rules, someone had to develop a simple but robust method for cleaning sprayers.
Continuous cleaning
In a later paper, the author and his team proposed a method called “Continuous cleaning” (download here), which employs a dedicated clean water pump to push spray solution from the tank and out the boom in the field. For comparison, the traditional triple rinse method employs the main pump to dilute the remaining spray solution with clean water in a series of rinses and sprays. You can learn more about point source contamination and rinsing methods in this clear and informative presentation by P. Balsari and P. Marucco (download here) given in 2015 at the University of Turin in Italy.
The continuous cleaning method isn’t new. In the 1970s some farmers cleaned their sprayers by plumbing a water supply hose into the suction line while spraying out the rinsate. They were on to something, because formal testing in the late 1990s showed that continuous cleaning was more efficient than triple rinsing. Then, from 2005 onward, research by groups such as betterspraying aps, TOPPS, the Julius Kuhn-Institut and AAMS further refined the process for both field and airblast sprayers.
Anderson et al. made compelling claims about the continuous cleaning method. They stated that a 4,000 L sprayer with a 400 L clean water reservoir would require only 100 L to clean the plumbing as effectively as triple rinsing, which would require the entire 400 L. The remaining 300 L could be used to rinse the exterior and the entire process could take place in the field, in rotating locations. Perhaps most intriguing of all was that it would only take five minutes.
But, it is important to note that their rinsate samples came from the nozzles, as required by France and Denmark. The issue of higher concentrations in dead-end plumbing is not addressed.
European adoption
In anticipation of the regulations, some manufacturers were already developing continuous cleaning kits to upgrade sprayers of all makes, models and ages. In Denmark (and to a lesser extent in France and Germany) these kits were used at workshops to upgrade sprayers. But, the installation process was not always straight-forward.
Some kits performed better than others and expertise was needed to match the flow rate, tank rinse nozzles and the pump’s power requirements to the sprayers. Depending on the sprayer’s design, it sometimes required trial and error to establish a process of opening and closing valves during rinsing. Independent testing showed that many sprayers were greatly improved,(download here) but others proved incompatible due to the volume or inaccessibility of residual spray mix remaining in the plumbing. Specific cases include dead-ends on boom sections, or exceptionally long return lines on circulating booms
Defining a fit for North America
In early 2016, we wrote a preliminary article describing what we knew of the method and it created a lot of interest. We decided to test it our for ourselves in a demo at the Canadian Outdoor Farm Show. But before we describe what we did, let’s clarify a few terms. You may have noted that in Europe the process is called “Continuous cleaning” but moving forward we will refer to the method as “Continuous rinsing”. This is because we feel cleaning a sprayer and rinsing a sprayer are different processes with different objectives.
“Cleaning” a sprayer is a total decontamination that should be performed when changing chemicals and at the end of every spray day. It requires the use of a detergent and any label-required additive (such as ammonia following the new dicamba products). Perhaps most importantly, it requires the operator to address the dead-end plumbing areas. There is no universally-accepted process, but we describe fairly common protocols for field sprayers here and for airblast sprayers here.
“Rinsing” is a less intensive process intended to reduce the amount of residue that can build up on, or soak into, sprayer surfaces. Water is brought into contact with most of the plumbing to dilute any solution left in the sprayer, and is then sprayed out in the field. This process should be performed every few loads, or when moving an empty sprayer between fields, or if the operator has (perhaps unwisely) decided not to clean the sprayer at the end of the day because they are spraying the same chemical tomorrow. Often, this is accomplished using the triple rinse process, which we describe here:
Triple Rinse Process
The pressure drops and nozzles sputter (i.e. spray tank is empty).
If the sprayer has an inductor bowl or loading bypass, and if the operator doesn’t already rinse these systems following filling, the operator will exit the cab, open the valve to clean water reservoir, and use a portion of the clean water to clean these circuits. In some cases, the rinse process can be performed without the operator having to leave the cab.
Sprayers with dead end plumbing on boom section ends warrant special consideration. Spray mix can be harboured in the dead ends and is a significant source of contamination, no matter how much rinsing is performed (see video). Therefore, the first rinse (step 5) should be interrupted before it is complete to allow boom ends to be opened, flushed and closed.
The operator then introduces 1/3 of the clean water reservoir to the spray tank through the rinsing nozzle(s) and circulates for 5 minutes (including the agitation line).
The operator returns to cab, and drives to spray the volume out in the field until the nozzles sputter.
Operator exits the cab and introduces 1/3 of the clean water reservoir to the spray tank through the rinsing nozzle(s) and circulates for 5 minutes (including the agitation line).
The operator returns to cab, and drives to spray the volume out in the field until the nozzles sputter.
Operator exits the cab and introduces 1/3 of the clean water reservoir to the spray tank through the rinsing nozzle(s) and circulates for 5 minutes (including the agitation line).
The operator returns to cab, and drives to spray the volume out in the field until the nozzles sputter.
The process, illustrated in this field sprayer plumbing animation, takes about 40 minutes and may require the operator to leave the cab multiple times.
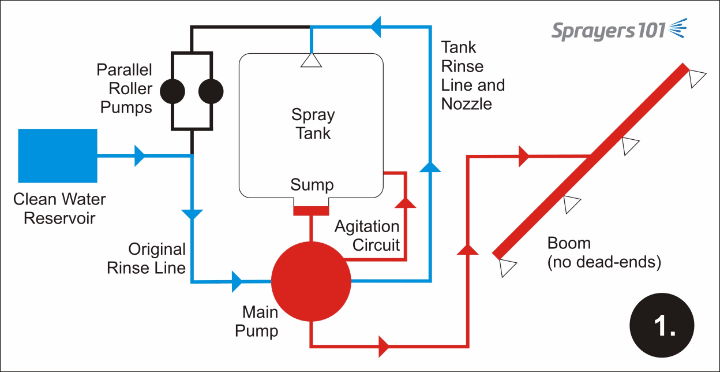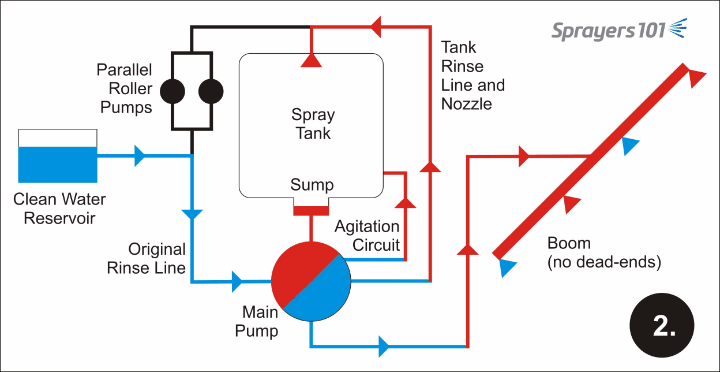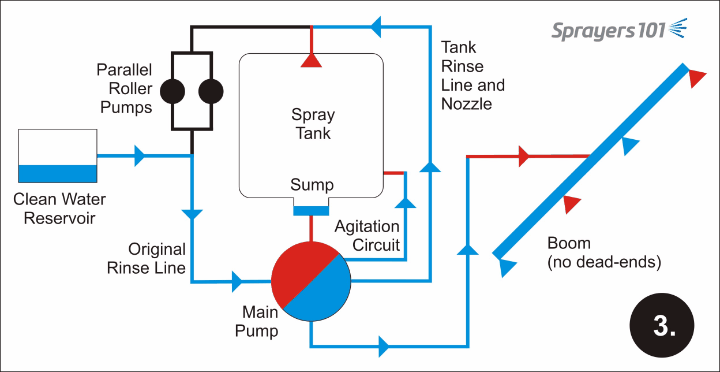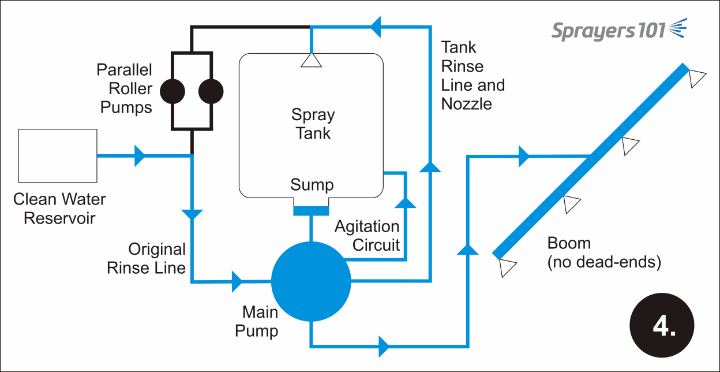
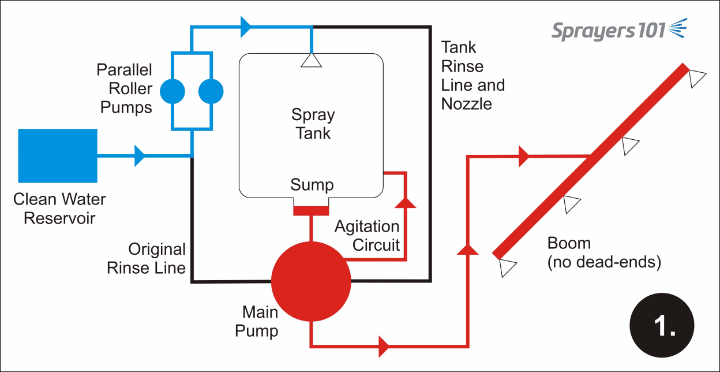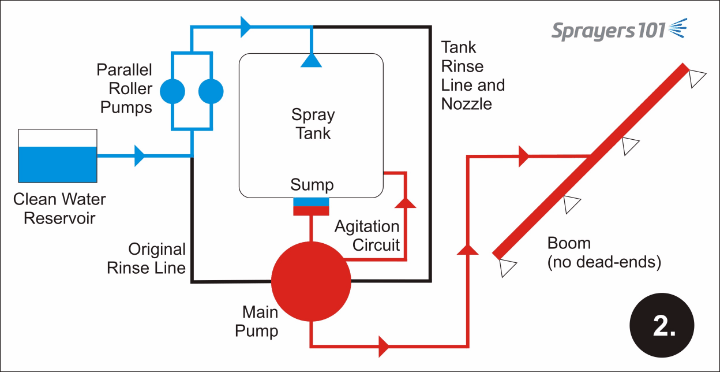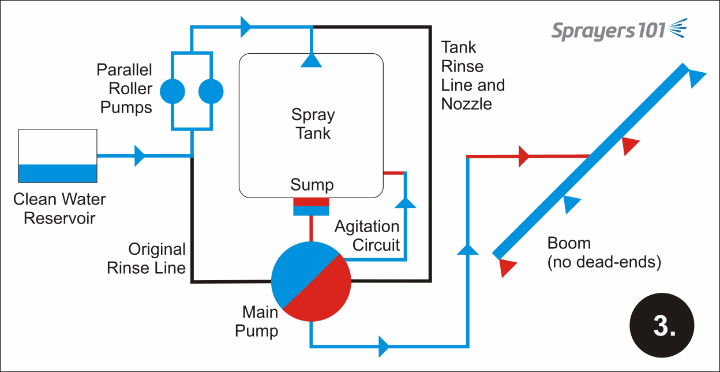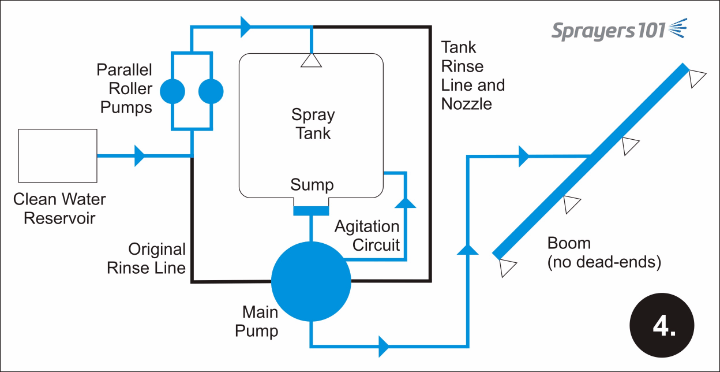
Continuous rinsing requires a second pump to be installed in the system. Rather than performing a serial dilution in three batches, this rinsing essentially pushes spray solution out of the sprayer using clean water. The agitation line creates some dilution since it loops back to the tank, but that small volume is quickly diluted by the process, as below:
Continuous Rinse Process
Pressure drops and nozzles sputter (i.e. spray tank is empty).
If the sprayer has an inductor bowl or loading bypass, and if the operator doesn’t already rinse these systems following filling, the operator will exit the cab, open the valve to clean water reservoir, and use a portion of the clean water to clean these circuits.
There can be no dead-end plumbing at the end of boom sections for this process to work (e.g. sections terminate with air-aspirating end caps).
The operator returns to cab (if they left), and begins introducing clean water to the tank through the rinsing nozzle(s).
When a small volume has been introduced, the operator engages the agitation line with reduced flow to tank and begins driving and spraying at a rate slightly higher than the clean water pump’s flow rate.
Operator continues to spray until the nozzles sputter.
The process, illustrated in this field sprayer plumbing animation, takes about 10 minutes and requires the operator to leave the cab once at most.
Building a demo system and model
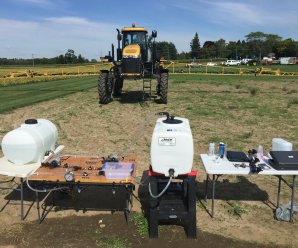
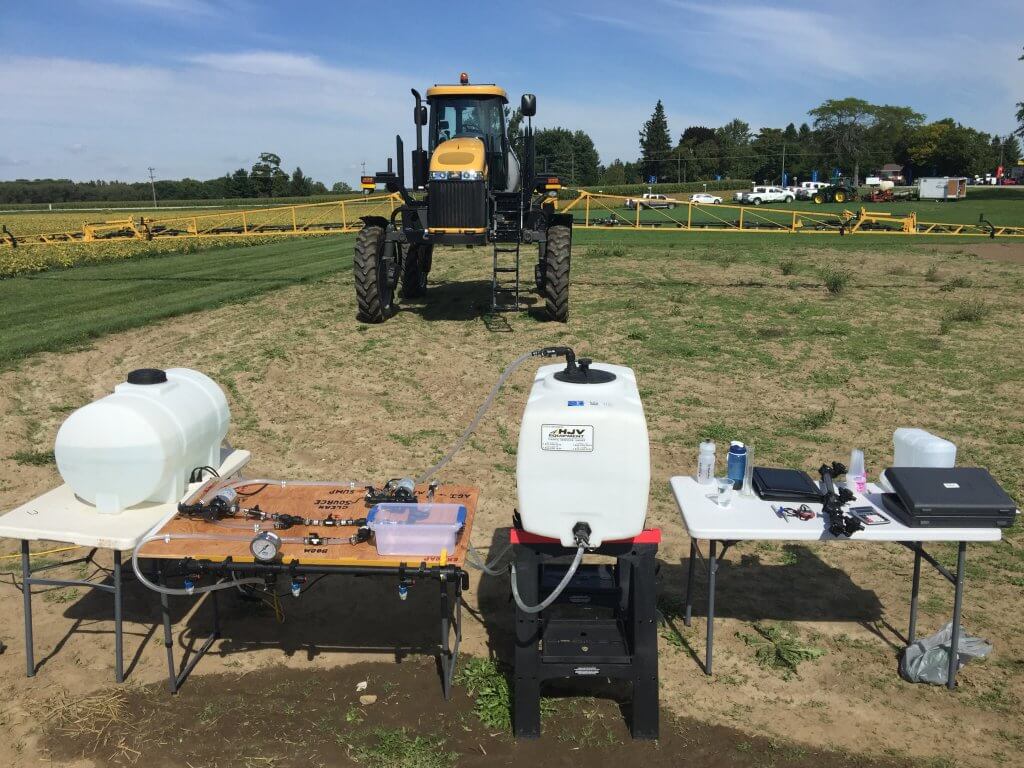
We worked with HJV Equipment in Alliston, Ontario to build a bench-top model representing a simple, scaled-down sprayer rinse system. Using the model, we planned to compare the effectiveness and the efficiency of triple rinsing to continuous rinsing – and we would do so in front of an audience. HJV felt that to make an appropriate model, we should base it on an installed system. So, they plumbed a working system into a RoGator 700.
They used two Hypro electric roller pumps (model 4101 N-H) in parallel, plumbed into the clean water reservoir. Anti-backflow valves led the water to the tank rinse nozzles. The system could be engaged from the cab and could be isolated from the existing rinse system, leaving the sprayer’s original system intact and available for when full cleanings were required. The designer/mechanic points out key features in the following video.
The RoGator 700 has a 700 US gallon tank and a 50 US gallon clean water reservoir. By tapping into an existing compressor, HJV created a means for blowing out the boom with air, greatly reducing the amount of spray solution left in the empty sprayer. Still, the “empty” sprayer would retain about 15 US gallons in the pump, sump and remaining lines. Based on those parameters, we designed and constructed our scaled model. We used 10 L in the main tank and 4.5 L in the clean water reservoir. The lines and sump held about 1.25 L so we felt breaking the 4.5 L of clean water into three 1.5 L volumes was fair.
In the images that follow you can see the components. Basically we have a spray tank, clean water reservoir, main pump, dedicated clean water pump, the sprayer boom, and some clever anti-backflow and valves to switch the “sprayer” from one method of rinsing to the next.
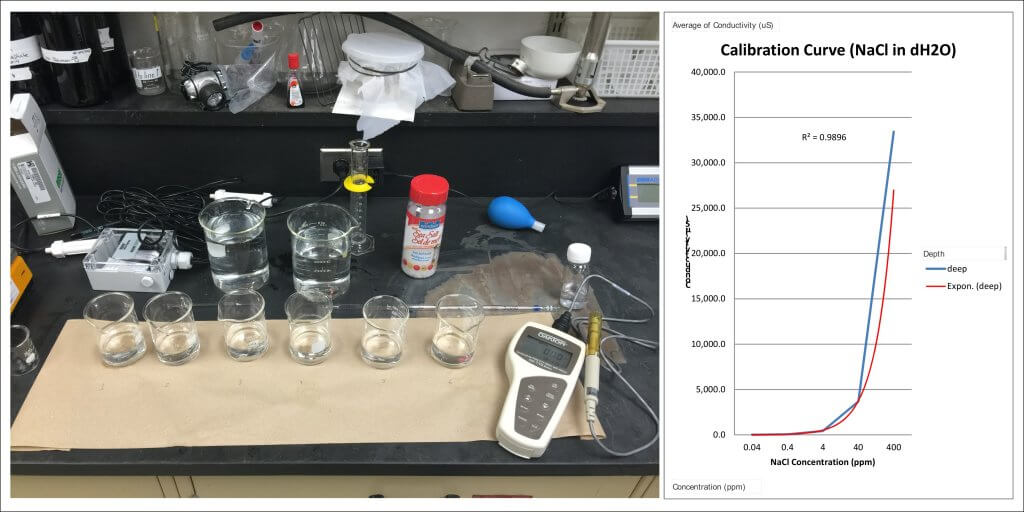
But, we still had to devise a means to measure the effectiveness of the two rinsing systems. UV dye would be difficult to use with a live audience in real time, and food colouring would be too subjective. We decided to use a conductivity meter, which quickly measures the electrical conductivity of a liquid. Using NaCl (table salt) as a readily-dissolved conductor, we calibrated the unit and found we could reliably register table salt in parts per million.
The demo process
We ran the demo six times over three days and recorded how long each rinse took and how effective each rinse was in reducing the original concentration. Here’s how we did it:
Triple Rinse (~4.5 minutes)
Fill the main tank to 10 L.
Introduce 10 cc of salt (and coloured with green food dye) to create our spray mix.
Circulate the solution through the main pump and agitation line to ensure it was completely homogeneous.
Start the system spraying out of the boom.
Draw a sample of the spray mix to serve as our baseline concentration.
When the nozzles began to sputter, the tank was “empty” (duration: 150 seconds).
We drained the boom via valve on the boom-end to simulate “blowing out” the boom. (duration: 5 seconds)
We introduced 1.5 L of clean water through the tank rinse nozzle (duration: 15 seconds).
We circulated the solution through the agitation line. (duration: 30 seconds).
We sprayed the solution out of the boom, drawing a sample of rinsate before the nozzles sputtered (duration: 30 seconds)
Repeat steps 8-10 two more times to represent the other two rinses.
Continuous Rinse (~1.5 minutes)
Fill the main tank to 10 L.
Introduce 10 cc of salt (and coloured with green food dye) to create our spray mix.
Circulate the solution through the main pump and agitation line to ensure it was completely homogeneous.
Start the system spraying out of the boom.
Draw a sample of the spray mix to serve as our baseline concentration.
When the nozzles began to sputter , the tank was “empty” (duration: 150 seconds).
We drained the boom via valve on the boom-end to simulate “blowing out” the boom. (duration: 5 seconds)
We reduced the agitation flow to a low rate and introduced 1.5 L of clean water through the rinse nozzle using our dedicated pump (duration: 5 seconds)
At the 5 second mark, we started spraying while still introducing clean water.
Samples of rinsate were drawn at regular intervals, with particular attention to collect the last volume fraction as the nozzles were sputtering (duration: 100 seconds)
Results
Triple Rinse
The average starting conductivity for the triple rinse demo was 2,520 µS (n=6). The final sample of rinsate registered a conductivity of 490 µS (n=6) representing a final concentration that was 19.4% of the original. Average time: 4.5 minutes.
Continuous Rinse
The average starting conductivity for the continuous rinse demo was 2,145 µS (n=6). The final sample of rinsate registered a conductivity of 342 µS (n=6) representing a final concentration that was 16% of the original. Average time 1.5 minutes.
We were surprised the model could not reduce the concentration of salt to an acceptable 1-2% level. The Agrimetrix Dilution Calculator App suggests it should have been much better. We suspect the standing volume of the system is higher than we predicted, and we weren’t using enough clean water to dilute it. We may have had better results if we’d used a lower concentration of salt to begin with, and/or a higher volume of clean water. We will continue to tweak the demo model and will update this article as we collect more information. The more stringent research in Europe showed that continuous rinsing is a effective as triple rinsing.
The most interesting result is that continuous rinsing took 1/3 of the time triple rinsing required (1.5 minutes versus 4.5 minutes). Research in Europe suggested 1/4 of the time as triple rinsing. The difference is likely accounted for by the time the operator used leaving and entering the cab.
You can see the effectiveness of the process in this AAMS demonstration video. Sure, their demo unit is nicer than the one we built, but our rustic version has charm 🙂 Note the sequence of opening and closing valves to ensure all circuits are rinsed clear of dye.
Conclusion
If continuous rinsing is as effective as triple rinsing and can be performed in a fraction of the time with less operator exposure, then we should be modifying our sprayers to support the method. Airblast sprayers and small field sprayers are relatively easy to modify, and can be even be equipped with a spray wand so excess clean can be employed to rinse down the exterior.
Larger field sprayers, however, may be more challenging as they do not all lend themselves to the conversion:
The clean water pump (hydraulic or electric) must have sufficient power.
Matching the pump capacity to the sprayer can be problematic; The clean water pump flow rate must be 30-50% of the boom flow rate.
Sprayers with dead-end boom sections or circulating-flow return lines may not be compatible, and those with pneumatic systems to clear the boom of solution are preferred.
More sophisticated electronic rate controller systems (e.g. on the larger self-propelled sprayers) may not be compatible.
And, of course, we must remember that neither triple or continuous rinsing should be seen as a replacement for the sprayer cleaning process. Any drain-able part of the sprayer will still harbour high concentrations of residues (e.g. filters, valves, inductors, bypass lines – any dead-end plumbing). With new stacked chemistries being introduced in North America (some still active when residues register as little as a few parts per million), diligent sprayer sanitation is more important than ever.
Thanks to Jan Langenakens of aams for his help researching and informing this article.
It’s been quite a ride. Here’s episode six of “Exploding Spray Myths”. Real Agriculture helps us share an important message about why sprayer clean out involves so much more than just the tank. If you think you know what we’re covered with, we’re accepting guesses.
And please, don’t blow into nozzles, even if they don’t touch your lips. Blowback is a real thing…
The first modern airblast sprayer was developed in the mid 1900’s, but competed with existing equipment before it was adopted by the majority. As you can see below, we’ve come a long way. As application technology continues to evolve and grow, so does the array of choices facing growers.
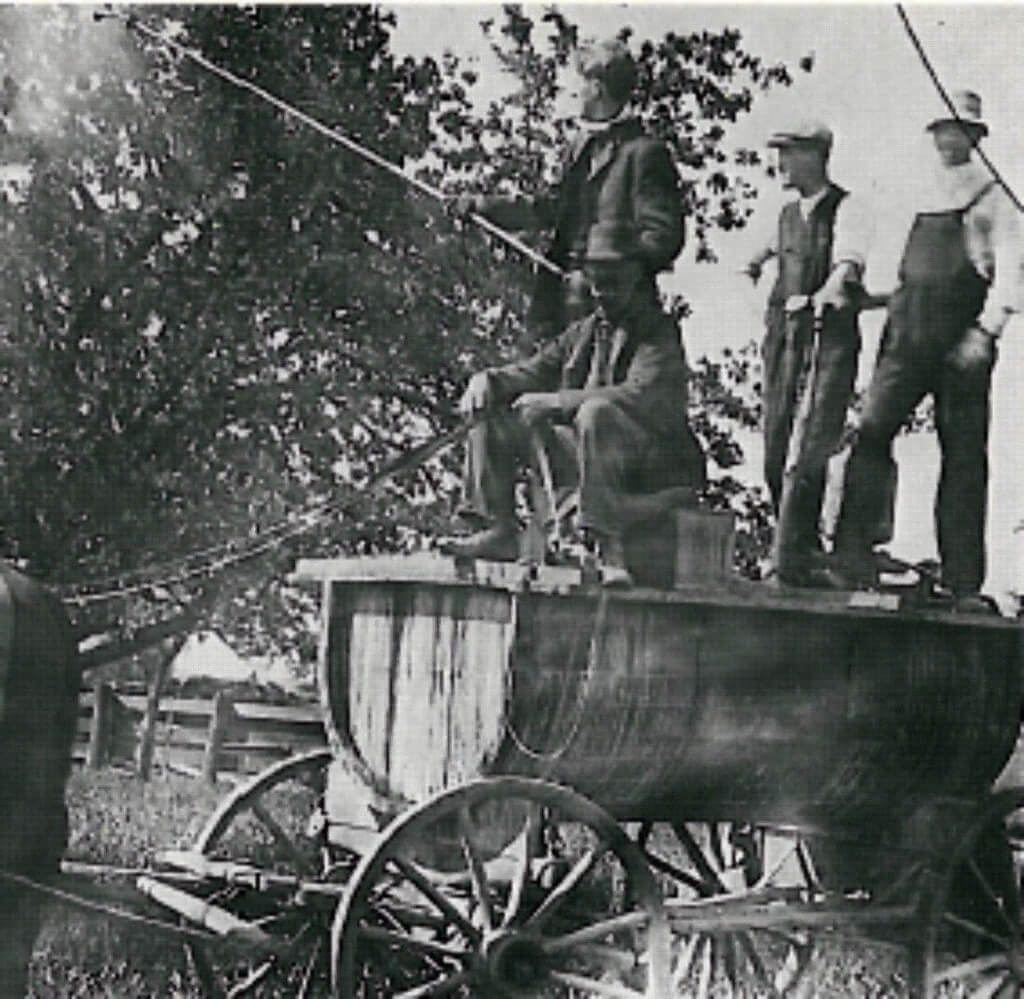
An Ontario orchard spray crew c.1910. Pump pressure was maintained by the two operators at the right. The spraying rate by the above method could cover 1.2 to 1.6 hectares (3 to 4 acres) per hour. Image from www.farms.com
Provide Agro (a subsidiary of N. M. Bartlett Inc.) had been considering introducing a new airblast sprayer to Canada for more than ten years. After deciding not to get into the manufacturing game, they explored importing sprayers from Europe and Australia. In late 2014 they recently invited me to see their choice: the H.S.S. CF airblast sprayer built by Holland-based “Hol Spraying Systems”.
It’s not often I get to see a “new” airblast sprayer design. To be fair, H.S.S. has been building similar sprayers in Holland for more than 20 years, so technically it was new-to-me.
We met at a local apple orchard in Simcoe, where we ran the sprayer through a series of light duties. The first thing we did was explore the sprayer’s features, both optional and standard. As the ambassador to Canada, this particular model had all the bells and whistles. Here is a list of features and observations I feel are worth relating. It’s important to note that this list is in no way an endorsement, nor are any omissions intended to be a condemnation.
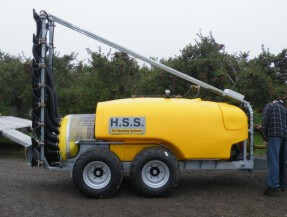
The H.S.S. CF sprayer. Outwardly this PTO-driven sprayer appears very different from Ontario’s typical fleet of airblast sprayers. Notably the flexible ducts and gantry comprising the tower, and the double axle. However, it operates using the same principles as our more familiar sprayers and following a brief inspection of welds and fastens (and given its more than 20 year history in Europe) it appears to be very durable.
Each duct is paired to a nozzle body, and that means each air outlet can be adjusted individually. The tower structure can be customized to match everything from vines to high-density orchards and even has an optional woolly aphid attachment for directing air and spray up-and-into the canopy. For taller crops like hops and semi-dwarf trees, a second fan can extend the tower to 5.5 m.
Anyone that’s been stuck in wet weather can appreciate the value in this adjustable double axle. Weight is distributed to reduce compaction and hopefully, the creation of ruts. This feature is standard, but you have the option to upgrade to hydraulic adjustment. I’m not sure how often an operator would want to adjust the axle length, but there it is.
The H.S.S. CF has a lot of features that promote operator safety by reducing the potential for exposure. One convenient feature is the access port separate from the tank fill port. No need to remove the basket to examine/clean the interior, and no need to remove the basket and come in contact with (potentially) concentrated pesticide residue.
Many large field sprayers feature tank rinse nozzles to facilitate sprayer cleanout following an application. Finally, airblast can boast this feature as well. The 150 L clean water tank supplies enough water to the tank rinse nozzles for a triple, low-volume rinse in the field with no need for a pressure washer or a nurse tank. This prevents residue buildup and reduces operator exposure – and it’s standard!
An optional feature is the tank level sensor, which can be tied to the agitation. If you are using a foamy tank mix, agitation won’t turn on until a preset tank level. I’m not certain about this option because proper tank suspension requires agitation from the beginning – just use a defoamer. Note the tank basket has a hose attached to the bottom… read on.
There’s a standard hydraulic jet at the bottom of the tank basket to assist in proper mixing. I don’t know if it precludes mixing a slurry, or if it will improve pesticide bag dissolution, but I have to assume it helps. I trust there’s a safety feature to prevent this nozzle from operating while the hatch is open, but I’m not certain.
This final standard feature may seem small, but it further reduces the potential for operator exposure. The onboard clean water source is separate from the spray tank and the tank-rinse supply and provides a convenient hand-wash station.
Other features include solenoid shut-offs for boom sections, a rate controller and a small-radius draw bar.
An important function of any airblast sprayer is air handling. Too often, tower sprayers have inconsistent air speeds (and presumably air volumes) over the length of the air outlet. Sometimes this can be compensated for using the small deflectors in the tower, or in extreme cases, replacing conventional hollow cone nozzles in “dead spots” with air induction hollow cones that produce coarser droplets and tend to fly farther under pressure. Using a Pitot meter, we examined the airspeed from each air outlet. The PTO was set to 400 rpm and the fan gear was in low.
Nozzle:
Ground
2
3
4
5
6
7
Top
Left
70 mph
85 mph
90 mph
85 mph
80 mph
85 mph
80 mph
85 mph
Right
75 mph
90 mph
90 mph
90 mph
80 mph
90 mph
85 mph
85 mph
There were no obvious dead spots, and the left and right sides of the tower seemed about equal. The bottom two positions were notably slower than the rest, but given the distance to the target in that position, and the fact that ambient wind is slower at the ground, it’s interesting, but not necessarily a concern.
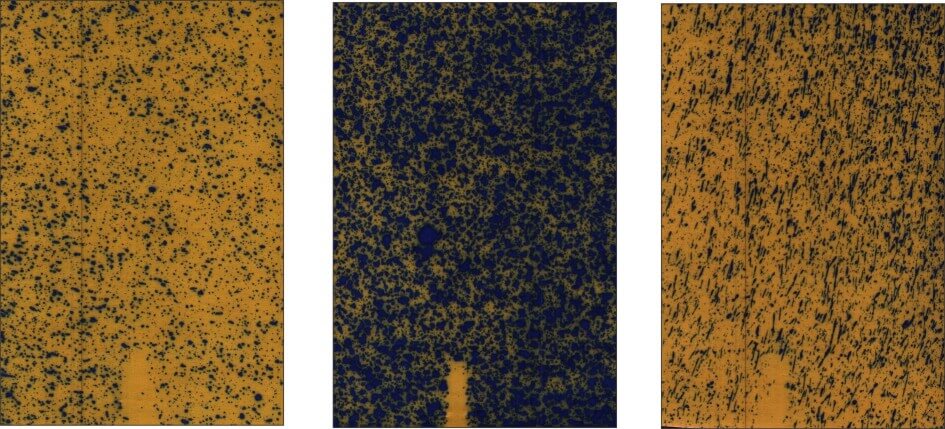
We arranged a set of water-sensitive targets in the canopies of semi dwarf apple trees to get a sense of the sprayer coverage. Admittedly, it was very humid and there was little wind that day, so coverage is much easier to achieve because so little spray evaporated or was blown off course before reaching the target. We ran different combinations of PTO speed and fan gear. These images are from 540 rpm and low fan gear using red Albuz nozzles (1.5 L/nozzle/minute @ 6 bar) spraying about 400 L/ha at about 5 kph. On a drier and windier day, higher volumes would be needed.
There were no obvious misses, even when papers were oriented parallel with the ground (exposing their narrow edge to the sprayer, such as in the paper on the right). This isn’t conclusive, but it does show that the sprayer had no trouble penetrating the canopy, and with further tweaking should be able to provide suitable coverage throughout the canopy. Personally, given the upward orientation, I would use the woolly aphid nozzle for all applications, particularly for drenches. More on that later.
One notable quality was the “quiet” operation of the sprayer. Applicators are familiar with the loud whine created by most airblast sprayers; at lower rpm’s and in low fan gear, the tractor seemed as loud (or even louder) than the sprayer operation. You can watch a video of one of the spray passes at the bottom of this article.
So the big question: “How much?”. You’ll have to contact the dealers to find out more, but I will say that stripped down to standard features, it’s comparable to some of the more expensive sprayers in Ontario. Don’t be dissuaded because I believe the expense is warranted given the features, with particular note of the on-board tank rinse system and adjustable air ducts.
So is this the sprayer for you? Well, if you’re in the market for a new sprayer, always start by prioritizing your goals. Perhaps work-rate is a priority, so look to sprayer capacity to reduce the number of refills and consider over-the-row technology (where possible) to reduce the number of passes. Perhaps the crop is adjacent to sensitive areas or residential homes and drift control is a priority; consider adjustable air direction and adjustable air speed.
When compiling a prioritized list, reflect on the positives and negatives of your current sprayer and talk to fellow growers about their experiences. It may come down to personal preference, but consider the following points. These points are in no particular order; they come from many articles I’ve read on the subject of considering new equipment purchases and from talking to dealers, mechanics and sprayer owners:
Necessity – Is a new sprayer really needed? Manufacturers have a number of retrofit kits available to upgrade and improve sprayers. If poor pesticide performance has led to the decision to purchase a new sprayer, be sure it’s related to the technology, and not to an operating error.
Crop Type and Acreage – Consider the size of the operation and the size, shape and density of the crop(s). Can the sprayer adapt to provide adequate coverage throughout the growing season and in the long-term? How flexible is the sprayer when spraying different products onto different targets? • Sprayer Capacity and Filling – Fewer refills means a higher work rate, but increased capacity also means more weight, so consider the effects on navigation, turning radius and soil compaction. Is the tank easy to fill?
Cleaning, Calibrating and Maintenance – Moving between crops sometimes requires complete cleaning and decontamination of the tank, lines, nozzles and any shrouds or ducts. Clean water reservoirs, tank-rinsing nozzles and overall accessibility should be considered. Review the steps required to winterize and to calibrate the sprayer. Is it easy to access parts? Is operator exposure minimized
Horsepower – This is an important consideration for airblast sprayers because fans move a lot of air and liquid. Tank agitators require power, too. Consider selecting from the higher range of manufacturer-recommended horsepower to improve longevity. Remember, however, that fans typically don’t have to operate at the maximum rated rpm’s, particularly early in the season.
Nozzle Technology and Operating Pressure – Consider the range of nozzle-types intended for use and ensure the sprayer can provide sufficient pressure. While more expensive, diaphragm and piston pumps have fewer moving parts in contact with the spray solution, reducing cleaning time and operator exposure.
Spraying Conditions – A sprayer has to be reliable, even in adverse conditions, so consider the operating environment. Night spraying, uneven terrain, high winds, dry conditions – many environmental factors can impact sprayer performance and may warrant special consideration. Investigate deflectors, shrouds and the structural framework and durability of the sprayer.
Since its introduction in late 2014, growers have been slowly adopting this sprayer in Ontario and the northern US. Some high-density operations have purchased the optional over-the-row boom system that allows them to spray multiple rows at once. Here at at the Simcoe Resource Station, we’re hoping to run the HOL sprayer in apples for the 2016 season to see if the optional woolly apple aphid (WAA) nozzle has any impact on scale, mites and of course, WAA control. Moreover, we plan to run that nozzle all season long to see if its upward angle improves underleaf coverage and canopy penetration.